
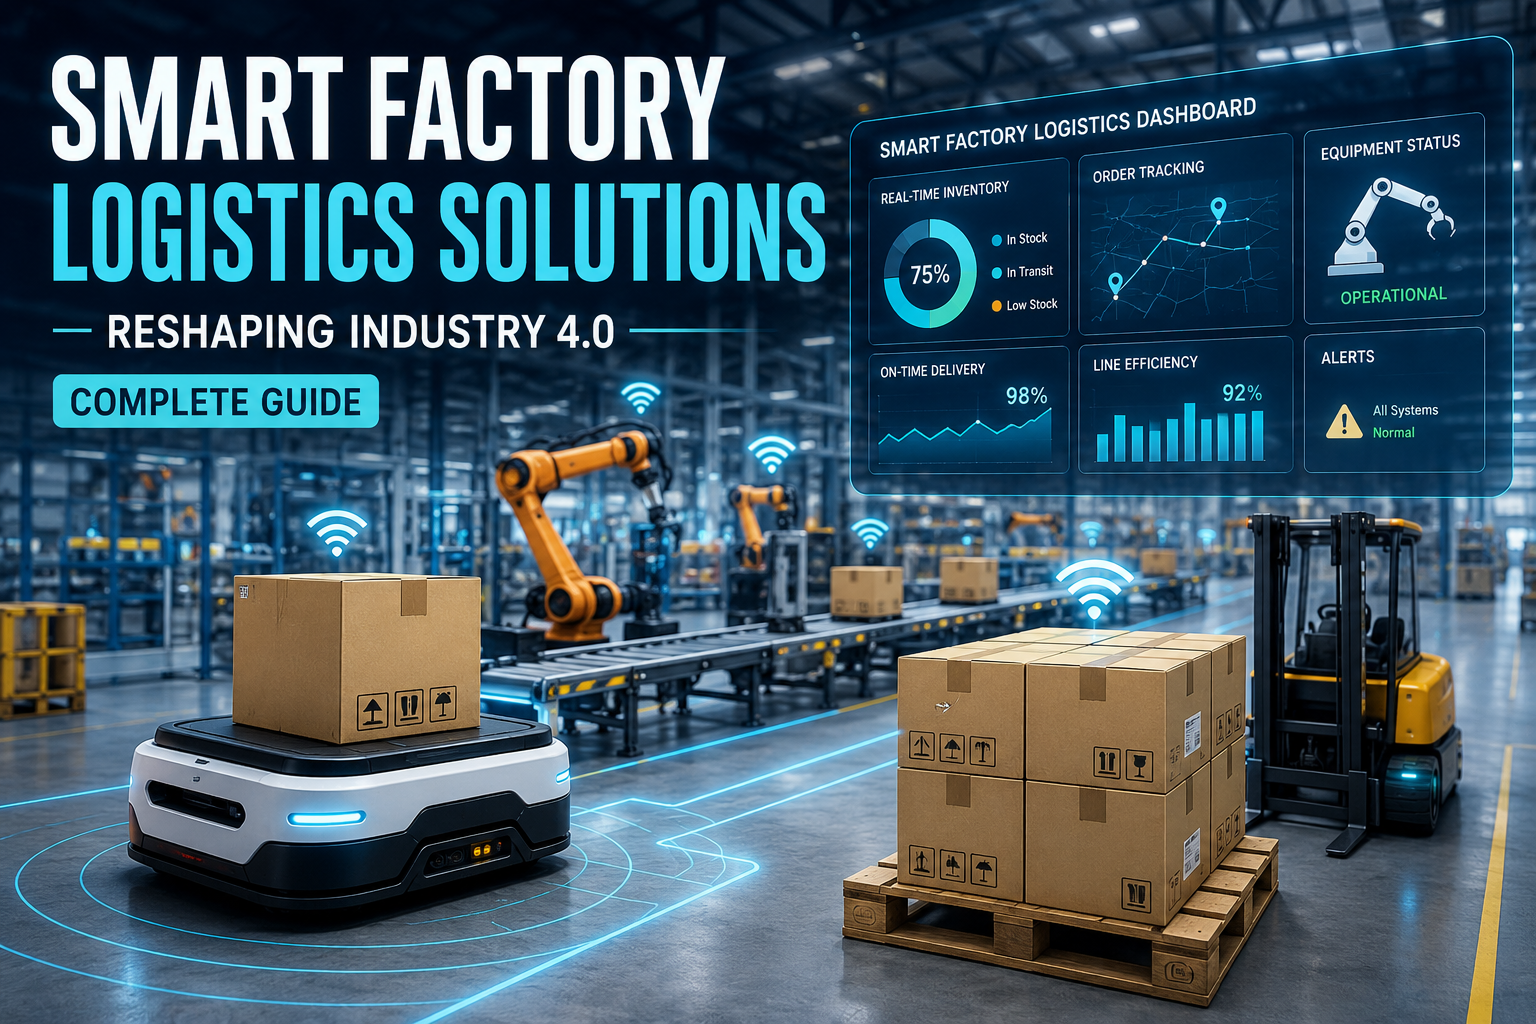
Smart factory logistics is no longer an experimental concept reserved for tech giants — it has become a core requirement for manufacturers who want to stay competitive. As production volumes grow and customer expectations shift toward faster, more accurate delivery, factories that still rely on manual tracking, disconnected systems, and reactive maintenance are falling behind.
At its core, smart factory logistics refers to the use of connected technology — sensors, software, robotics, and data analytics — to manage the movement of materials, information, and finished goods across a manufacturing operation. It merges the physical factory floor with digital intelligence, allowing every part of the production and distribution process to communicate in real time.
In this guide, we’ll break down what smart factory logistics actually involves, the technologies driving it, the measurable benefits it delivers, and a practical roadmap for adopting smart factory logistics solutions in your own operation.
What Is Smart Factory Logistics?
Smart factory logistics is the integration of Industry 4.0 technologies, including IoT sensors, AI, robotics, and cloud software, into the material handling, inventory, and distribution functions of a factory. Unlike traditional logistics, it connects every stage of production into a single data system. This is part of the broader shift toward Industry 4.0 logistics, where machines, software, and people share information continuously. As a result, problems like delayed shipments, bottlenecks, or failing machines can be spotted and fixed early.
If your team is exploring where to start, our warehouse automation services page shows how this connects to inventory and fulfillment.
Why Smart Factory Logistics Matters Right Now
Manufacturing has entered a period where efficiency gains from traditional lean methods are plateauing. McKinsey’s ongoing research into advanced manufacturing has found that factories deploying Industry 4.0 use cases have achieved measurable gains — including double-digit improvements in overall equipment effectiveness through better analytics and problem-solving — showing that data-driven operations consistently outperform manual ones. You can read more in McKinsey’s report on advanced manufacturing and Industry 4.0.
Separately, Deloitte’s ongoing smart factory research has tracked how digitally connected manufacturers are pulling ahead of competitors still running fragmented, manual logistics operations — a gap explored further in Deloitte’s Industry 4.0 and connected manufacturing insights.
Three forces are accelerating adoption:
- Rising customer expectations for faster, more transparent delivery timelines
- Labor shortages on the factory floor that make automation a necessity, not a luxury
- Supply chain volatility that punishes companies without real-time visibility
Key Technologies Behind Smart Factory Logistics Solutions
Modern smart factory logistics solutions are built on a handful of core technologies. Understanding each one helps clarify where to focus your investment.
IoT in Factory Logistics
IoT in factory logistics is the connective layer that makes everything else possible. Sensors attached to machines, pallets, forklifts, and storage racks continuously transmit data — location, temperature, vibration, usage cycles — to a centralized platform.
This constant flow of data means factory managers no longer have to physically walk the floor to know where materials are or whether equipment is functioning normally. Instead, dashboards display live conditions across the entire facility, and alerts flag anomalies the moment they occur.
Alt text suggestion: “IoT sensors tracking smart factory logistics inventory in real time”
AI-Driven Factory Logistics
AI-driven factory logistics takes the raw data collected by IoT sensors and turns it into actionable insight. Machine learning models can forecast demand fluctuations, optimize delivery routes within the plant, and flag inefficiencies that would be nearly impossible for a human to spot manually across thousands of data points.
For example, AI can analyze historical order patterns to predict which materials will be needed on the line next week, automatically triggering procurement before a shortage occurs.
Predictive Maintenance Logistics
Predictive maintenance logistics uses sensor data and machine learning to anticipate equipment failures before they happen, rather than reacting after a breakdown halts production.
Traditional maintenance schedules are based on fixed time intervals, regardless of actual equipment condition. Predictive maintenance flips this model: it monitors vibration, temperature, and performance data continuously, alerting maintenance teams only when the data indicates a genuine risk of failure. This reduces both unnecessary maintenance costs and unplanned downtime.
Smart Warehouse Logistics
Smart warehouse logistics extends these same principles into storage and fulfillment. Automated guided vehicles (AGVs), robotic picking systems, and RFID tracking replace manual inventory counts and forklift routing with systems that self-optimize based on real-time demand.
A smart warehouse doesn’t just store goods — it actively manages inventory placement, predicts restocking needs, and coordinates with production schedules so materials arrive exactly when they’re needed, not before or after.
Benefits of Smart Factory Logistics
The benefits of smart factory logistics extend well beyond simple cost-cutting. Manufacturers who adopt these systems typically see improvements across four key areas:
- Reduced downtime — predictive maintenance and real-time monitoring catch problems before they stop production
- Lower operating costs — automated material handling reduces labor overhead and minimizes waste from overstocking or understocking
- Faster order fulfillment — connected systems eliminate the delays caused by manual handoffs between departments
- Improved decision-making — centralized data gives managers a single source of truth instead of conflicting reports from disconnected systems
- Greater supply chain resilience — real-time visibility allows faster response to disruptions, from supplier delays to demand spikes
These benefits compound over time. A factory that starts with basic IoT tracking often finds it has the data foundation needed to layer on AI-driven forecasting and predictive maintenance within a year or two — without needing to rebuild its systems from scratch.
How Smart Supply Chain Management Connects to Factory Logistics
Smart supply chain management and smart factory logistics are closely linked but not identical. Factory logistics focuses on what happens inside the plant — material flow, machine coordination, internal transport. Supply chain management extends that visibility outward to suppliers, distributors, and customers.
When these two systems are connected, a factory can automatically adjust internal production schedules based on incoming supplier data, or notify distribution partners the moment a batch is ready to ship. This end-to-end connectivity is what separates a truly “smart” operation from one that has simply automated a few isolated tasks.
How to Implement Smart Factory Logistics Solutions: A Step-by-Step Approach
Adopting smart factory logistics doesn’t require replacing your entire operation overnight. A phased approach tends to produce better results and lower risk.
- Audit your current logistics workflow. Identify where delays, manual handoffs, and data blind spots occur most frequently.
- Start with IoT sensor deployment. Begin tracking high-value or high-risk assets — this creates the data foundation for everything that follows.
- Centralize your data. Route sensor and system data into a single dashboard or platform rather than letting it sit in disconnected silos.
- Introduce predictive analytics. Once you have reliable historical data, layer in AI models for maintenance forecasting and demand planning.
- Automate material handling gradually. Pilot AGVs or robotic picking in one zone before scaling facility-wide.
- Connect internal logistics to your broader supply chain. Share relevant data with suppliers and distribution partners to close the loop.
- Review and refine continuously. Smart factory logistics is not a one-time project — ongoing tuning based on real performance data is what delivers long-term ROI.
Common Challenges in Adopting Smart Factory Logistics
No transformation is without friction. The most frequently reported obstacles include:
- Legacy system integration — older equipment often lacks the connectivity needed for IoT sensors, requiring retrofitting
- Upfront investment — sensors, software, and automation hardware require capital that can be difficult to justify without a clear ROI model
- Workforce adaptation — employees need training to work alongside automated systems rather than being replaced by them
- Data security — connecting factory equipment to networks introduces cybersecurity considerations that weren’t relevant in isolated, offline systems
Addressing these challenges early — particularly through a phased rollout rather than a full-scale overhaul — significantly improves the odds of a successful transformation.
The Future of Smart Factory Logistics
Smart factory logistics is moving toward tighter links between physical operations and digital intelligence. Digital twins, which are virtual copies of production lines, let manufacturers test logistics changes before applying them on the factory floor. AI is also shifting from simple alerts to autonomous decisions, like rerouting materials without waiting for human approval. Factories that build a strong data foundation now, starting with IoT and predictive maintenance, will be ready for these next steps.
Frequently Asked Questions
What is smart factory logistics?
>>>>>>>>>Smart factory logistics uses connected technologies like IoT sensors, AI, and robotics to manage the flow of materials and finished goods inside a factory in real time.
What are the main benefits of smart factory logistics?
It reduces downtime, lowers operating costs, speeds up order fulfillment, improves decision-making, and makes the supply chain more resilient.
How is smart factory logistics different from smart warehouse logistics?
Smart factory logistics covers the entire manufacturing operation, including production line material flow and machine coordination. Smart warehouse logistics is a subset focused specifically on storage, inventory management, and fulfillment within warehouse facilities.
Related Guides
- Smart Connected Factory: The Core Technologies
- How to Modernize Your Automation Systems
- Workflow Automation Consulting: How It Improves Efficiency