
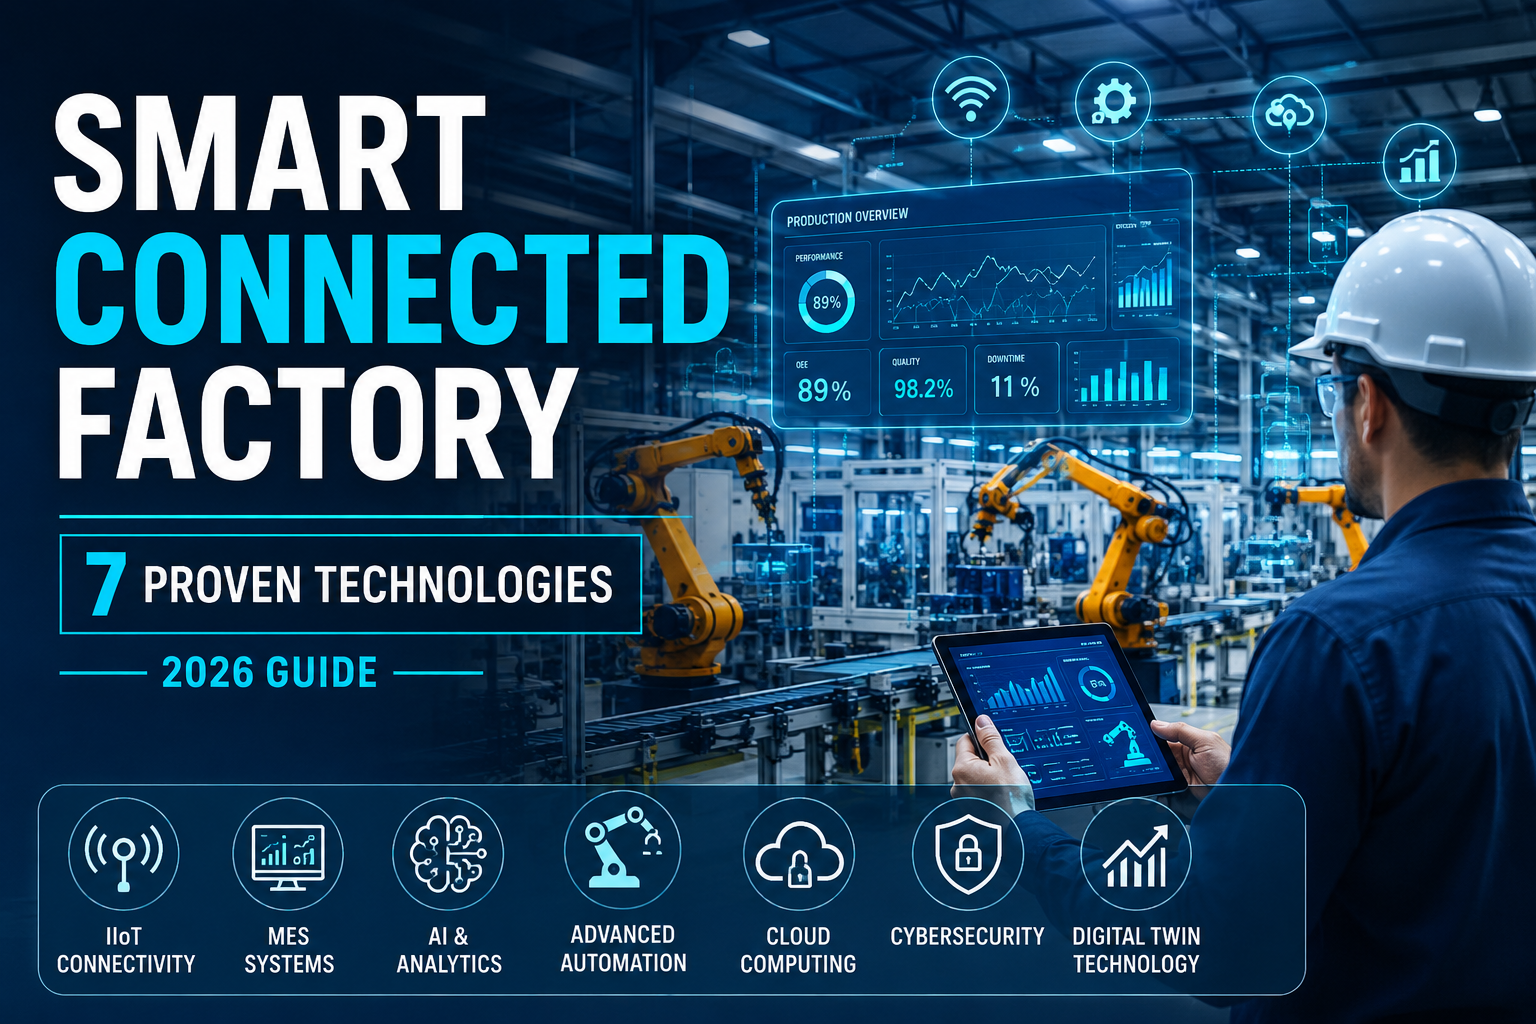
A smart connected factory links machines, sensors, software, and people through a continuous data loop. This setup helps manufacturers make decisions in minutes instead of waiting a week. Manufacturers now need this technology to stay competitive.
According to McKinsey & Company research, global manufacturers that implement smart factory technologies have achieved productivity gains of up to 30% and reduced downtime by nearly 50% through predictive maintenance and automation. These improvements help factories lead their markets and compete with faster, more efficient businesses.
In this guide, we’ll break down exactly what a smart connected factory is, the core technologies behind it, the measurable benefits, the real challenges you’ll face, and how to actually get started. If you’re evaluating smart factory solutions for your own operation, this is the deep-dive competitors haven’t written.
What Is a Smart Connected Factory?
A smart connected factory is a manufacturing facility where machines, sensors, software systems, and workers are digitally linked, allowing data to flow in real time across the entire production environment. Unlike a traditional factory — where information about a machine fault, a quality defect, or a supply shortage might take hours to reach the right person — a smart connected factory surfaces that information instantly, often with automated recommendations attached.
The concept builds directly on Industry 4.0 smart factory principles: cyber-physical systems, the industrial internet, and data-driven decision-making. But a smart connected factory isn’t just about installing sensors. It’s about creating a closed loop between the physical shop floor and the digital systems that plan, monitor, and optimize it.
At its core, a smart connected factory combines three layers:
- Connectivity — sensors, PLCs, and edge devices that capture data from machines and processes
- Intelligence — software that analyzes that data (AI, analytics, machine learning)
- Action — automated or human-guided responses that improve output, quality, or uptime
When all three layers work together, you get a factory that doesn’t just report what happened — it predicts what’s about to happen and helps you act on it.
Why Smart Connected Factories Matter for Industry 4.0
Manufacturing has always generated data — machine logs, quality checks, inventory counts. What’s changed is the ability to connect, analyze, and act on that data in real time, at scale.
According to Deloitte’s 2025 Smart Manufacturing Survey, the vast majority of manufacturers now view smart manufacturing as the primary driver of competitiveness over the next three years — not a side initiative, but the core strategy. That’s a meaningful shift from a decade ago, when digital transformation projects were treated as optional pilots.
The pressure driving this shift is practical, not theoretical:
- Labor shortages are forcing plants to do more with fewer skilled workers on the floor.
- Supply chain volatility means manufacturers need real-time visibility, not weekly reports.
- Customer demands — especially in aerospace, medical devices, and automotive — increasingly require digital traceability that paper records simply can’t provide.
A connected factory doesn’t just make operations faster. It makes them resilient, auditable, and adaptable to conditions that change week to week rather than year to year.
There’s also a widening gap between intent and execution worth watching. A large majority of manufacturing operations leaders plan to increase digital and AI investment over the next five years, yet only a small fraction report those technologies fully embedded across all operations today. That gap is exactly where competitive advantage lives — the manufacturers who close it first, rather than just planning to, are the ones capturing the productivity gains described above.
This is also why the “smart connected factory” label matters more than it might seem. A factory with a handful of disconnected sensors isn’t the same thing as one with unified connectivity across IIoT, MES, and analytics. The value doesn’t come from any single piece of technology — it comes from how well those pieces are integrated with each other.
Core Smart Factory Solutions Powering Connected Production
A smart connected factory is built from several interlocking technologies. Here are the ones doing the heaviest lifting.
Industrial IoT (IIoT) Platform
An industrial IoT (IIoT) platform is the connective tissue of the smart factory. It’s the software layer that ingests data from sensors, PLCs, and legacy machines, then standardizes that data so other systems — analytics tools, dashboards, MES — can actually use it.
Without an IIoT platform, most factories end up with data trapped in silos: one system for machine uptime, another for quality, another for inventory, none of them talking to each other. A good IIoT platform solves that by acting as a single source of truth for shop floor data, regardless of which vendor made the underlying equipment.
Manufacturing Execution System (MES)
A manufacturing execution system (MES) sits between your ERP (which plans production at a business level) and your machines (which actually build the product). MES software tracks work orders, manages quality checks, records genealogy and traceability data, and gives supervisors a live view of what’s happening on every line.
In a smart connected factory, MES is where IIoT data becomes operational decisions — turning a stream of sensor readings into a scheduling adjustment, a quality hold, or a maintenance ticket.
Edge Computing in Manufacturing
Not all data can wait for a round trip to the cloud. Edge computing in manufacturing processes data locally, right at the machine or on the factory floor, so time-sensitive decisions — like stopping a line before a defect propagates — happen in milliseconds instead of seconds.
Edge computing also reduces bandwidth costs and keeps critical operations running even if a plant’s internet connection drops, which matters more than most buyers initially expect.
Computer Vision and Quality Inspection
Increasingly, smart connected factories are layering computer vision onto their IIoT platforms for automated quality inspection. Vision systems can detect defects with accuracy approaching 99.5%, compared to roughly 80–90% for manual inspection on repetitive tasks. That gap compounds fast on high-volume lines, where even a small increase in missed defects translates into significant scrap and rework costs.
Combined with an IIoT platform and MES, computer vision doesn’t just catch defects — it feeds that data back into root-cause analysis, helping engineering teams identify which machine, shift, or material batch is driving quality issues.
Predictive Maintenance Software: Reducing Downtime in Real Time
Predictive maintenance software helps smart connected factories detect equipment problems early. It uses sensor data and machine learning to predict failures and reduce downtime.
These programs can deliver returns of 10:1 to 30:1 within 12 to 18 months, according to the provided content. Predictive maintenance also helps manufacturers improve efficiency and reduce repair costs.
Digital Twin Manufacturing: Simulating the Factory Floor
Digital twin manufacturing creates a virtual copy of a machine, production line, or factory using real-time sensor data. Engineers can test changes and maintenance plans in this virtual model before applying them to physical equipment.
This approach saves time and money while reducing production risks. Digital twins are now widely used in manufacturing to improve efficiency and decision-making.
Common use cases include:
- Simulating layout changes before a physical retooling
- Testing new product variants virtually before committing floor space
- Running “what-if” scenarios for capacity planning
- Validating process changes against quality requirements before rollout
Ye short version hai. Main important keywords aur information same rakhi hai.
Real-Time Production Monitoring for Smarter Decisions
Real-time production monitoring displays sensor and MES data on live dashboards. Supervisors can track OEE (Overall Equipment Effectiveness), throughput, and downtime as they happen.
According to McKinsey’s Industry 4.0 research, one white-goods manufacturer increased OEE by 11% through better machine alarm monitoring and data analytics, without adding new hardware.
Live alerts also help operators detect machine problems early. They can prevent defects, reduce downtime, and improve production.
Benefits of a Smart Connected Factory
Pulling these technologies together delivers benefits that compound across the operation:
- Higher productivity — connected operations combining IIoT, robotics, and real-time data commonly deliver productivity gains between 15% and 30% within the first few years of implementation.
- Reduced downtime — predictive maintenance and automated monitoring catch problems before they become stoppages.
- Better quality control — computer vision and connected quality checks catch defects with far higher consistency than manual inspection alone.
- Improved supply chain visibility — connected systems give planners real-time insight into inventory, work-in-process, and supplier status.
- Faster, more accurate decision-making — Industry 4.0 technologies have been shown to improve supply chain forecasting accuracy substantially, replacing guesswork with data.
- Energy and resource optimization — connected sensors help identify waste in energy, materials, and machine cycles that would otherwise go unnoticed.
For a deeper breakdown of how these gains translate into ROI for your specific operation, see our [Industry 4.0 ROI calculator] — link this to a relevant page on your site.
Challenges to Building a Smart Connected Factory
None of this happens without friction. Manufacturers considering a smart connected factory should plan for these obstacles upfront:
- Legacy equipment integration — older machines weren’t built with connectivity in mind, and retrofitting sensors onto decades-old equipment takes real engineering effort.
- Cybersecurity exposure — every connected sensor is a potential entry point for attackers, and industrial control systems are increasingly targeted. NIST has published dedicated cybersecurity guidance specifically for manufacturing control systems to help plants manage this risk.
- Skilled labor gaps — running and maintaining a connected factory requires workers who understand both operations technology (OT) and information technology (IT), a skill combination that’s still in short supply.
- Data silos and system fragmentation — without a unifying IIoT platform, connected factories can end up with more data but no clearer picture, if systems aren’t integrated properly.
- Upfront investment — while ROI is strong, the initial cost of sensors, platforms, and integration work requires a clear business case and phased rollout plan.
Working through these challenges systematically — rather than trying to connect everything at once — is what separates successful smart factory rollouts from stalled ones.
How to Get Started With Smart Factory Solutions
You don’t need to digitize your entire operation on day one. A phased approach works better in practice:
- Start with one high-impact use case — predictive maintenance on your most critical asset is usually the fastest win.
- Choose an IIoT platform that integrates with your existing equipment rather than requiring a full hardware replacement.
- Add real-time production monitoring so teams can see the value of connected data immediately.
- Layer in MES once you have reliable real-time data flowing, to turn insights into standardized workflows.
- Expand to digital twin modeling for capacity planning and process testing once your data foundation is solid.
- Build cybersecurity into every phase, not as an afterthought once systems are already connected.
Frequently Asked Questions
What is a smart connected factory?
A smart connected factory links machines, software, and workers to share real-time data and improve production.
How is a smart connected factory different from a traditional smart factory?
A traditional smart factory focuses on one facility. A connected factory links multiple facilities and business systems.
What technologies are required to build a smart connected factory?
Key technologies include IIoT, MES, edge computing, predictive maintenance software, and digital twins.
How much does it cost to implement a smart connected factory?
Costs depend on factory size, connected machines, sensors, and hardware needs.
What is the ROI of predictive maintenance in a smart connected factory?
It can deliver returns of 10:1 to 30:1 within 12 to 18 months, according to the provided content.
Is cybersecurity a bigger risk in a smart connected factory?
Yes. Connected machines face more cyber threats, so manufacturers need strong security controls.
Related Guides
- Smart Factory Logistics: A Complete Guide
- How to Modernize Your Automation Systems
- How to Program LED Displays: A Beginner-to-Advanced Guide